

Choosing ffs packaging for global buyers involves more than comparing film prices or machine speed. The right format must protect products, run reliably, and fit local supply chains. A bag that performs well in a dry warehouse may wrinkle, leak, or lose seal strength in tropical conditions. Small details matter, including gusset design, filling accuracy, seal temperature, and pallet stability.
Industry data shows why this decision deserves careful review. The OECD’s Global Plastics Outlook reports that global plastic waste more than doubled from 2000 to 2019, while only about 9% was recycled. This pressure is reshaping packaging specifications. Smithers’ The Future of Flexible Packaging to 2028 also identifies sustainability, lightweighting, and improved barrier performance as major market drivers. However, “sustainable” does not always mean suitable. A thinner film can reduce material use, but it may increase punctures or product loss during transport.
Global buyers should therefore evaluate ffs packaging through real operating conditions, not brochures alone. Ask for seal-strength data, oxygen and moisture barrier results, drop-test evidence, and machine compatibility records. Check whether the film remains stable after long-distance shipping. Test samples with the actual product. This is essential.
There is no universal winner. A recyclable mono-material structure may support future recovery goals, yet it can require tighter temperature control on the filling line. A high-barrier laminate may offer stronger protection, but recycling options can be limited. The best choice balances product safety, production experience, regional requirements, and measurable environmental performance. Some assumptions will be wrong. Testing exposes them early.
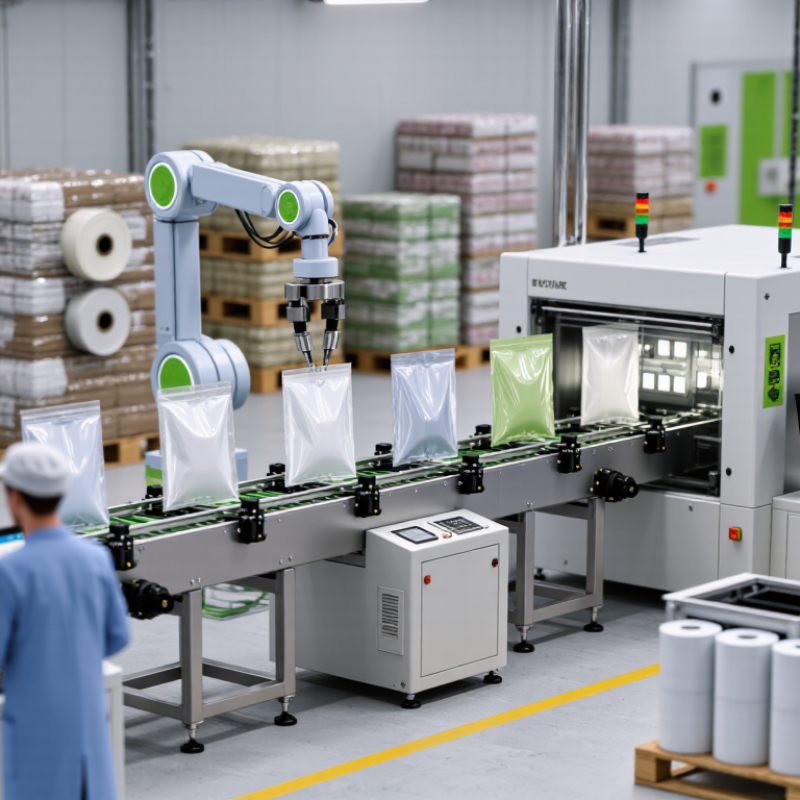
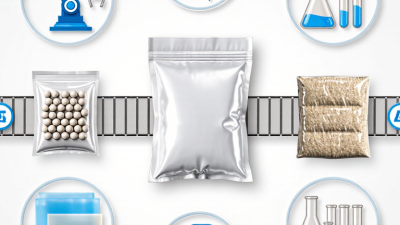
Choosing FFS packaging starts with the product, not the machine. VFFS packaging forms bags vertically from a roll of film. It suits powders, grains, snacks, pet food, and free-flowing solids. The product drops from above, while the film is shaped and sealed below. This layout saves floor space and supports high output. However, dusty powders may affect seal areas. A reliable trial should test filling accuracy, seal strength, and film behavior.
HFFS packaging forms and seals packs horizontally. It works well for cookies, bars, medical supplies, and products needing gentle handling. The product travels through the machine on a flat path. This helps protect delicate items from vertical drops. HFFS can also create pillow packs, three-side seals, and shaped pouches. Yet, the equipment usually needs more space and careful product spacing. Small differences matter.
Sachet packaging is a practical choice for single-use products. It fits liquid condiments, instant drink powders, creams, and measured doses. Sachets support portion control and convenient distribution across markets. For liquids, seal design and viscosity testing are essential. For powders, dust control becomes critical. I have seen attractive samples fail during transport because their seals were too weak. That mistake is easy to repeat. Buyers should check barrier performance, filling tolerance, local recycling requirements, and temperature conditions before approving the FFS format. A sample may look perfect. Production is less forgiving.
| Product Type | Recommended FFS Format | Typical Package Style | Common Fill-Weight Range | Suitable Product Characteristics | Typical Film Requirements | Main Advantages | Key Selection Considerations |
|---|---|---|---|---|---|---|---|
| Powders and fine dry mixes | VFFS | Pillow bag, gusseted bag, or brick-style bag | 50 g–5 kg, depending on machine configuration | Free-flowing or semi-free-flowing powders such as flour, spices, drink mixes, and powdered ingredients | Heat-sealable laminate with adequate moisture, oxygen, and aroma protection; anti-static performance may be useful | Efficient vertical filling, compact equipment footprint, and good suitability for multiple bag sizes | Dust control, seal contamination, product aeration, and accurate auger or volumetric dosing must be evaluated |
| Granules, grains, and pellets | VFFS | Pillow bag, gusseted bag, or block-bottom bag | 100 g–10 kg or more for larger industrial bags | Free-flowing products such as rice, pulses, seeds, sugar, pet food, and plastic pellets | Heat-sealable polyethylene-based films or laminated structures selected for strength, puncture resistance, and moisture protection | High throughput, flexible bag dimensions, and compatibility with multihead or linear weighing systems | Particle size distribution, drop impact, abrasion, dust generation, and seal strength affect final performance |
| Liquid and viscous products | VFFS or HFFS | Three-side-seal pouch, four-side-seal pouch, or formed sachet | 5–500 ml for small and medium retail formats | Sauces, dressings, concentrates, gels, detergents, and other pumpable products | Liquid-compatible heat-sealable laminate with strong seals and suitable chemical resistance | Portion control, low material usage, and convenient single-use distribution | Filling temperature, viscosity, splash control, leak testing, and seal-area cleanliness are critical |
| Single-use powders and liquid portions | Sachet packaging | Three-side-seal, four-side-seal, or stick sachet | 1–50 g or 1–50 ml for typical single-dose applications | Condiments, instant beverages, pharmaceutical powders, sweeteners, cosmetics, and sample quantities | High-barrier laminate when protection from moisture, oxygen, light, or aroma loss is required | Low unit cost, compact shipping, easy distribution, and precise portioning | Choose sachet geometry according to dose, product flow, opening method, tear performance, and required barrier level |
| Snack foods and irregular solid pieces | VFFS | Pillow bag, gusseted bag, or quad-seal bag | 20 g–1 kg | Chips, nuts, dried fruit, confectionery, and other lightweight or fragile pieces | Flexible laminate with grease, moisture, and oxygen protection; puncture resistance is important for sharp-edged products | Fast weighing and filling, attractive retail presentation, and broad size flexibility | Product breakage, headspace, static, film stiffness, and nitrogen-flushing requirements should be tested |
| Bars, biscuits, and flat products | HFFS | Flow-wrap pack with fin seal and end seals | 10–500 g per pack | Snack bars, cereal bars, biscuits, wafers, soap bars, and other products with a stable length and shape | Heat-sealable film selected for machinability, printability, grease resistance, and required barrier performance | Good product presentation, controlled orientation, high-speed wrapping, and convenient tear-open formats | Product dimensions, spacing, alignment, seal temperature, and film coefficient of friction must match the wrapper |
| Fragile or pre-formed products | HFFS | Flow-wrap, pillow-style horizontal pack, or sealed tray overwrap | 20 g–1 kg | Bakery products, fragile confectionery, medical disposables, and products requiring controlled horizontal handling | Flexible film with suitable stiffness, puncture resistance, and barrier protection for the product’s shelf-life needs | Gentler product handling, accurate positioning, and strong visual presentation | Conveyor transfer, product spacing, infeed design, and protection against compression or vibration are important |
| Fresh produce and products requiring gas flushing | VFFS or HFFS | Modified-atmosphere pouch, pillow bag, or flow-wrap pack | 100 g–2 kg | Salads, fresh-cut produce, bakery items, and products whose shelf life can benefit from controlled gas composition | Film must provide the appropriate balance of oxygen and carbon-dioxide transmission, sealability, and moisture management | Potential shelf-life improvement, reduced handling, and efficient retail packaging | Film permeability, product respiration, gas-flush accuracy, condensation, and cold-chain conditions must be validated |
| Frozen foods and moisture-sensitive products | VFFS | Pillow bag, gusseted bag, or resealable bag | 250 g–5 kg | Frozen vegetables, frozen fruit, ice products, and dry foods requiring strong moisture protection | Low-temperature heat-sealable film with high puncture resistance and strong moisture-barrier properties | High production efficiency and suitability for a wide range of retail and food-service pack sizes | Seal performance at low temperatures, frost contamination, impact resistance, and storage conditions require testing |
| Medical, pharmaceutical, and personal-care portions | Sachet packaging or HFFS | Four-side-seal sachet, stick pack, or single-item flow-wrap | 1–100 g or 1–100 ml | Wipes, creams, gels, powders, tablets, and controlled-dose personal-care or healthcare products | Validated barrier laminate or medical-grade film, with controlled seal integrity and traceability requirements | Hygienic single-use presentation, accurate dosing, and compact global distribution | Regulatory requirements, cleanroom controls, tamper evidence, seal validation, and lot traceability may apply |
Buyer note: VFFS forms and seals bags in a vertical direction and is generally preferred for free-flowing powders, granules, liquids, and irregular products. HFFS forms and seals packs horizontally and is generally preferred for bars, biscuits, fragile items, and products requiring controlled orientation. Sachet packaging is a small-dose package format that can be produced using either vertical or horizontal forming equipment. Actual fill-weight limits, speed, film structure, and barrier performance depend on the product, package dimensions, dosing system, and local regulatory requirements.